Depamu High-Quality Helical Rotor Pump for Viscous Liquids: A China Manufacturer Profile
In the global landscape of fluid transfer equipment, the efficient handling of highly viscous liquids has long posed significant engineering challenges. Industries ranging from petrochemical refining to food processing routinely require pumps capable of moving thick, shear-sensitive, and often abrasive media without compromising product integrity or operational reliability. Among the solutions that have proven particularly effective in addressing these demands is the helical rotor pump, also known as the progressing cavity pump. This article examines the helical rotor pump technology offered by Depamu (Hangzhou) Pumps Technology Co., Ltd., a prominent Chinese manufacturer that has integrated advanced German engineering principles with domestic manufacturing scale to serve a worldwide clientele.
Company Background and Positioning
Depamu (Hangzhou) Pumps Technology Co., Ltd., established in 2003 and headquartered in the Qiantang Area of Hangzhou, operates as a high-tech enterprise specializing in the research, development, production, and sales of a diverse range of fluid transfer equipment. The company's product portfolio encompasses Metering Pumps in plunger, mechanical diaphragm, and hydraulic diaphragm configurations; high-pressure process Reciprocating Pumps; pneumatic Diaphragm Pumps; Screw Pumps in single, double, and triplex screw designs; rotor pumps with both metal and rubber options; anti-corrosion centrifugal pumps; and cryogenic pumps. This breadth of offerings positions Depamu as a comprehensive supplier capable of addressing multifaceted fluid handling requirements across numerous industries.
The company's commitment to technological advancement is evidenced by its successful application for over one hundred technical patents since its founding. Depamu has obtained certifications from the American Petroleum Institute (API), the European CE marking system, ISO 9001 for quality management, ISO 14001 for environmental management, and ISO 45001 for occupational health and safety management. Notably, the company serves as a drafter of pump industry standards in China, a role that underscores its technical authority and influence within the sector.
The Helical Rotor Pump: Technical Principles and Advantages
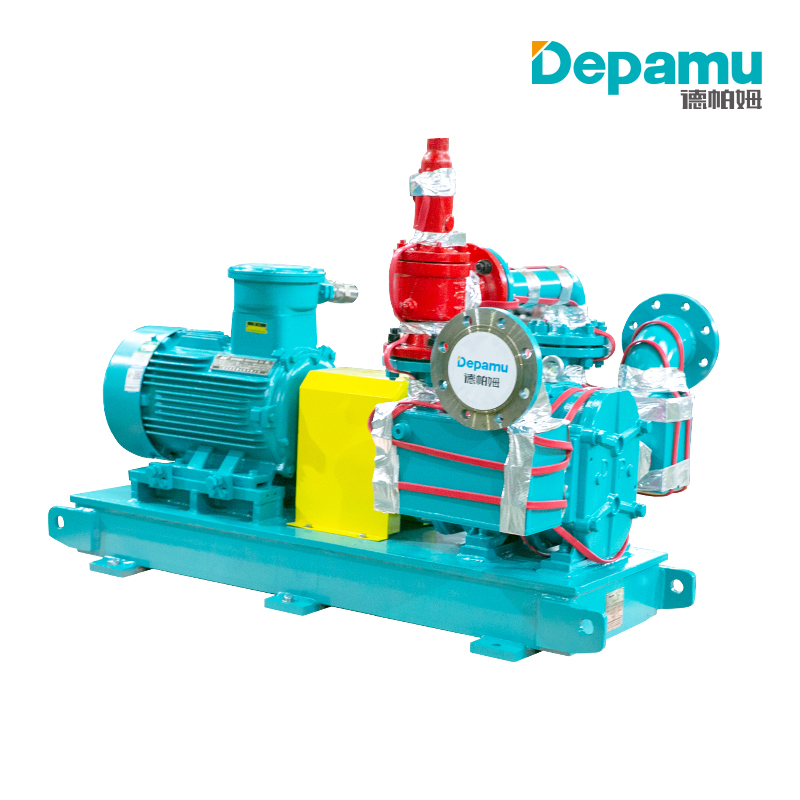
The helical rotor pump, frequently referred to as a progressing cavity pump, belongs to the category of positive displacement pumps. Its fundamental design comprises two principal components: a rotating helical rotor and a stationary stator with a corresponding helical bore. The rotor, typically a round-threaded screw, is attached on one side in either a hinged or elastic manner. As the rotor turns within the stator, it creates a series of sealed cavities that progress from the suction end toward the discharge end of the pump. These cavities, isolated from one another by the continuous line of contact between the rotor and stator, trap a fixed volume of fluid and force it through the pump without the pulsation and turbulence characteristic of many other pump types.
This operating principle confers several significant advantages for viscous liquid applications. The pump's low internal velocity and gentle handling minimize shear stress on the pumped medium, making it suitable for fluids whose molecular structure or physical properties might be compromised by more aggressive pumping mechanisms. The pump chambers maintain a constant shape and volume during operation, which ensures consistent volumetric delivery regardless of viscosity variations. Furthermore, the helical rotor pump exhibits excellent self-priming capability, capable of lifting fluids from depths without the need for external priming equipment or auxiliary devices.
Depamu's Helical Rotor Pump Specifications
Depamu's rotor pump line is engineered to meet the demanding requirements of high-viscosity fluid transfer. The company's pumps are designed in accordance with the API 676 standard, the American Petroleum Institute's specification for positive displacement rotary pumps. This compliance signals adherence to internationally recognized criteria for design, materials, manufacturing, and testing.
The performance envelope of Depamu's rotor pumps is substantial. The pumps are capable of transporting media with a viscosity of up to two million centipoise (cP), a figure that encompasses substances ranging from heavy crude oils and molasses to certain types of sludge and polymer solutions. The flow rate capacity spans a broad range from 0.1 to 3,000 cubic meters per hour, accommodating both small-scale dosing applications and large-volume transfer operations. The maximum suction head lift reaches nine meters, further enhancing operational flexibility.
The pumps demonstrate exceptional tolerance for solids-laden media, able to handle a solid content of up to sixty percent by volume. Incompressible particles with diameters of up to eighty millimeters can pass through the pump without obstruction, a capability that proves invaluable in wastewater treatment, mining, and food processing contexts where media frequently contain foreign matter. The double support structure employed in Depamu's rotor pumps provides enhanced mechanical stability, enabling output pressures of up to 1.8 megapascals, with multistage configurations reaching 3.0 megapascals.
Design and Manufacturing Quality
The quality of Depamu's helical rotor pumps is rooted in a combination of advanced manufacturing techniques and meticulous component design. The rotors and other critical components are produced using three-dimensional flow finishing dies and five-axis linkage machining techniques, processes that yield high efficiency with low noise generation. The axial and radial bushings are manufactured from wear-resistant and corrosion-resistant materials, contributing to extended service life and reduced maintenance frequency.
The pumps operate at rotational speeds between 10 and 650 revolutions per minute, a relatively low range that minimizes wear on the rotor and stator surfaces while preserving the integrity of shear-sensitive media. This low-speed operation, combined with the gentle pumping action inherent to the progressing cavity design, makes Depamu's rotor pumps particularly suitable for applications involving flammable chemical liquids and other hazardous materials that require careful handling.
Maintenance considerations have been incorporated into the design philosophy. The compact structure of the pumps minimizes the number of consumable components and reduces the frequency of failures. The pumps are engineered to permit online repair and maintenance without necessitating the dismantling of the associated pipeline system, a feature that translates directly into reduced downtime and lower operational costs. The positive inversion function allows the pumps to operate in reverse, which facilitates rapid clearance of blockages and further enhances practical usability.
Applications Across Industries
The versatility of Depamu's helical rotor pumps is reflected in the breadth of their application. In the petroleum and petrochemical sector, the pumps are employed for the transfer of crude oil, slurry oil, and residual oil, as well as for offshore oil pollution recovery and emergency rescue operations. The ability to handle mixed media containing solids, liquids, and gases with minimal pulsation is particularly advantageous in these contexts.
Water treatment and environmental engineering constitute another significant area of application. The pumps are used in drinking water supply systems, wastewater treatment plants, and sludge handling facilities, where their capacity to manage high solid content and fibrous materials proves essential. In the food and beverage industry, the gentle, low-shear pumping action preserves product quality during the transfer of viscous liquids such as juices, syrups, and pastes. The chemical fiber, resin, and pulp and paper industries also benefit from the pumps' ability to handle thixotropic and abrasive media without degradation of either the product or the equipment.
Global Reach and Client Base
Depamu has established itself as a trusted partner to some of the largest industrial enterprises in China and beyond. The company maintains long-term strategic partnerships with major entities including the China National Petroleum Corporation (CNPC), the China Petroleum & Chemical Corporation (SINOPEC), the China National Offshore Oil Corporation (CNOOC), and the China National Nuclear Corporation (CNNC). These relationships attest to the reliability and performance standards that Depamu's products consistently meet.
The company's export footprint extends to over fifty countries and regions, including the United States, the United Kingdom, France, and other established industrial markets. This international presence demonstrates that Depamu's helical rotor pumps are competitive not only on the basis of cost but also in terms of technical performance and compliance with rigorous international standards.
Service and Support
Depamu supplements its manufacturing capabilities with a comprehensive after-sales service infrastructure. The company offers a 7-day, 24-hour service line and maintains service stations positioned to respond promptly to customer requirements. In the event of an equipment fault or technical query, Depamu guarantees activation of a response mechanism immediately upon receipt of the customer's report, with a corresponding solution provided within twenty-four hours. Where necessary, after-sales personnel can be dispatched to the project site to assist with troubleshooting at the owner's request. This level of service commitment is particularly valued in industrial contexts where unplanned downtime carries significant financial and operational consequences.
Conclusion
Depamu (Hangzhou) Pumps Technology Co., Ltd. represents a compelling example of how a Chinese manufacturer has leveraged advanced engineering principles, rigorous quality management, and scalable production capabilities to deliver helical rotor pumps that meet the exacting demands of international industry. The company's rotor pumps, compliant with API 676 standards and capable of handling viscosities up to two million centipoise and solid contents of sixty percent, offer a robust solution for the most challenging viscous liquid transfer applications. With a global customer base, comprehensive certifications, and a demonstrated commitment to service excellence, Depamu continues to strengthen its position as a significant player in the worldwide pump manufacturing sector. For industries seeking reliable, efficient, and cost-effective solutions for viscous fluid handling, Depamu's helical rotor pumps merit serious consideration.